A 3D transfer bag may look intact, yet a tiny defect can compromise an entire fluid transfer. That is why every procedure should begin with a clear question: How to perform a leak test on a 3D transfer bag? The answer depends on the bag design, material, connection type, and approved testing method.
Richard Denk, a recognized single-use bioprocessing specialist, states, “A leak test is only as reliable as the method, equipment, and acceptance criteria behind it.” This principle matters in real operations. A calibrated pressure gauge, clean test area, and documented acceptance limit are essential. The operator should inspect the film, ports, seals, tubing, and protective packaging before testing. Look closely at folded corners. Check around welded seams. Small wrinkles can hide weak points.
A controlled pressure-decay test is commonly used when the bag supplier provides suitable parameters. Some facilities may use an approved immersion or bubble-based method for specific components. The selected method must follow the manufacturer’s instructions and site procedures. Never guess the test pressure. Excessive pressure can damage the bag and create a false result.
Record the bag identification, test equipment, pressure, duration, temperature, and outcome. A second inspection can prevent avoidable mistakes. Still, the process is not flawless. Environmental temperature, operator handling, and sensor accuracy may affect the result. If pressure drops unexpectedly, stop the transfer and investigate before release. A passing test supports confidence, but it does not replace sound handling, validated procedures, or careful judgment.
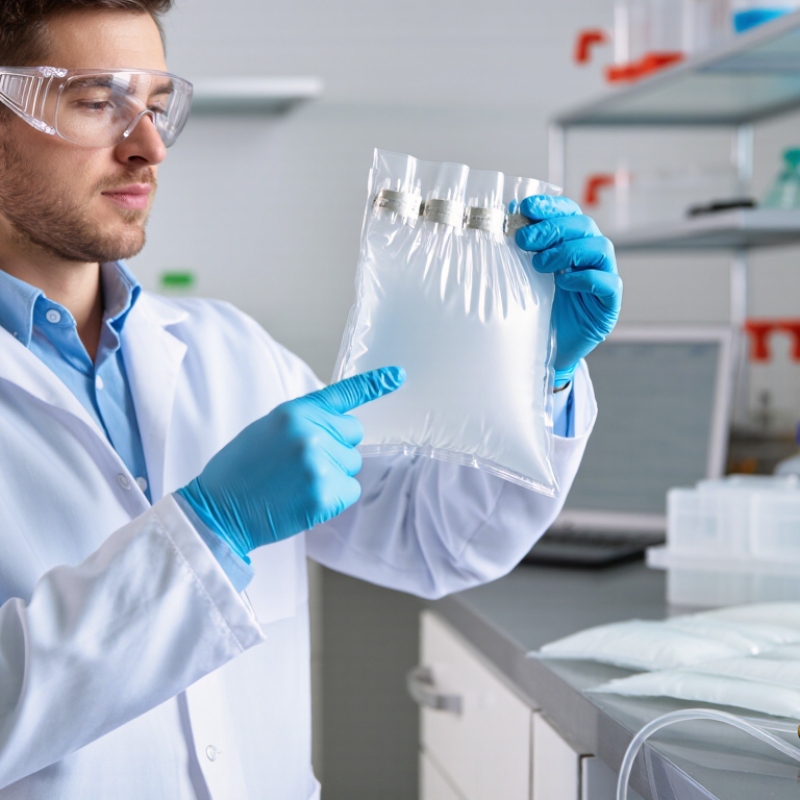
Prepare the 3D Transfer Bag and Leak-Test Equipment
Before testing, inspect the 3D transfer bag under bright, angled light. Check the film, seams, ports, clamps, and protective caps for creases, scratches, or loose connections. Review the batch number and sterilization record against the approved manufacturing documents. BioPhorum’s 2023 single-use systems survey identified integrity assurance and documentation as persistent industry concerns. That matches practical experience: small connector defects can remain invisible during a quick visual check.
Prepare a calibrated pressure gauge, regulated test gas, tubing, and a timer. Confirm that the equipment’s calibration status is current. Use the pressure range and hold time defined in the validated procedure; never copy values from another bag size. USP <1207.1> emphasizes method suitability, equipment control, and documented test conditions for package integrity testing. Keep the bag on a clean, flat surface, away from sharp edges. Support the ports gently.
Connect the test line without stressing the film. Close unused ports with verified caps or clamps. Record the starting pressure, ambient temperature, test duration, and final pressure. A stable reading supports integrity, but it does not replace visual inspection. FDA’s aseptic processing guidance also stresses controlled handling and documented contamination-control practices. I still recheck the fittings after setup. It is easy to miss one. If pressure changes unexpectedly, stop, inspect every connection, and repeat only under the approved investigation process.
Inspect the Bag, Ports, Tubing, and Seals Before Testing
How to Perform a Leak Test on a 3D Transfer Bag?
Inspect the bag under bright, angled light. Look for pinholes, cloudy film, creases, or stretched corners. Run clean fingers along every seal. Do not test a bag with visible damage. Check each port for cracks, loose caps, and distorted welds. Tubing deserves close attention. Small cuts can hide beneath clamps. Confirm that every connection is fully seated and capped before pressurization.
Use a validated pressure and hold time from your site procedure. Never copy values from another bag design. Temperature changes can alter pressure readings. ASTM F2096 describes bubble testing for gross leaks, but it does not prove microbial integrity. USP <1207.1> recommends deterministic container-closure methods when practical. Helium testing is often associated with leak rates near 10⁻⁶ mbar·L/s, yet that value is not a universal acceptance limit. The material, volume, and process define the correct criterion.
Pressurize gradually and watch the seals, ports, and tubing junctions. A stable gauge is useful, but it is not enough. Apply an approved leak-detection solution only when compatible with the bag material. Continuous bubbles indicate a leak. Record pressure, duration, temperature, operator, and bag identification. PDA Technical Report No. 66 emphasizes documented integrity controls across handling and transport. In practice, I would repeat a failed test after checking the fixture. Sometimes the fixture leaks. That detail is easy to miss. Never squeeze the bag aggressively; artificial stress can create a misleading result.
Connect the Test System and Apply Controlled Pressure
Connect the 3D transfer bag to a calibrated leak-test system using clean, compatible tubing. Check that the fittings are fully seated and the clamps are secure. A loose connection can imitate a bag leak. Record the equipment identification, test date, and operator name before applying pressure.
Use the pressure range and hold time defined in the approved procedure. Increase pressure slowly, rather than opening the regulator fully. Watch the gauge as the bag expands into a smooth, supported shape. Do not stretch the film or press the bag against sharp edges. Once the target pressure is reached, close the valve and allow a short stabilization period. Temperature changes can affect the reading.
Look closely at the seals, ports, and corners during the hold period. A stable gauge is useful, but it is not the only evidence. Some systems also monitor pressure decay electronically, which can improve repeatability. In practice, I recheck every connection before rejecting a bag. I once found a minor fitting gap that looked like a failed seal. That mistake changed my inspection routine. If pressure drops beyond the acceptance limit, stop the test, identify the cause, and document the result. Never compensate by raising pressure beyond the validated limit. Safety comes first.
How to Perform a Leak Test on a 3D Transfer Bag? - Connect the Test System and Apply Controlled Pressure
Controlled-Pressure Leak Test Record for a Flexible 3D Transfer Bag
| Test No. |
Test Stage |
Parameter |
Acceptance Criteria |
Recorded Value |
Status |
| 1. Test System and Bag Identification |
| 01 |
Bag identification |
Bag configuration |
Three-dimensional flexible transfer bag with all ports and seals intact |
3D transfer bag; single-use assembly; ports capped before testing |
Pass |
| 02 |
Test system connection |
Connection arrangement |
Pressure source, calibrated gauge, isolation valve, and test connector securely connected |
Connected to the designated test port; all unused ports capped |
Pass |
| 03 |
Instrumentation check |
Pressure gauge range and resolution |
Gauge range suitable for the test pressure; resolution no greater than 1 mbar |
0–600 mbar range; 1 mbar resolution |
Pass |
| 04 |
Environmental condition |
Test room temperature |
18–25 °C, with no direct heating or cooling applied to the bag |
22.1 °C |
Pass |
| 2. Controlled Pressure Application |
| 05 |
Initial inspection |
Visual condition before pressurization |
No visible punctures, open seams, damaged ports, or displaced clamps |
No visible defects observed |
Pass |
| 06 |
Pressure application |
Pressure increase rate |
Increase pressure gradually to avoid sudden stress on the film and seals |
Approximately 25 mbar/s |
Pass |
| 07 |
Target pressure |
Applied gauge pressure |
Reach the validated test pressure without exceeding the approved bag limit |
300 mbar(g) |
Pass |
| 08 |
Pressure stabilization |
Stabilization period |
Allow the bag and gas temperature to stabilize before starting the timed hold |
5 minutes |
Pass |
| 09 |
Bag condition under pressure |
Expansion and surface condition |
Uniform expansion with no abnormal bulging, hissing sound, or visible deformation |
Uniform expansion; no abnormal deformation or audible leakage |
Pass |
| 3. Pressure-Hold Leak Evaluation |
| 10 |
Pressure-hold start |
Starting pressure |
Record pressure after stabilization and before isolating the test system |
300 mbar(g) |
Pass |
| 11 |
Pressure-hold duration |
Timed hold period |
Maintain the isolated bag at the validated pressure for the defined test duration |
10 minutes |
Pass |
| 12 |
Pressure-hold end |
Ending pressure |
Pressure loss must remain within the approved limit |
299 mbar(g) |
Pass |
| 13 |
Pressure decay |
Pressure loss during hold |
Not greater than 5 mbar over 10 minutes |
1 mbar over 10 minutes |
Pass |
| 14 |
Pressure decay rate |
Calculated decay rate |
Not greater than 0.5 mbar/min |
0.1 mbar/min |
Pass |
| 15 |
Leak localization check |
Connections, ports, seams, and film surfaces |
No visible bubbles or continuous leakage indication when checked with a compatible leak-detection method |
No bubbles or leakage indication observed |
Pass |
| 4. Test Completion |
| 16 |
Depressurization |
Pressure release |
Release pressure slowly and safely through the designated vent or test connection |
Pressure reduced gradually to atmospheric pressure |
Pass |
| 17 |
Post-test inspection |
Bag and connection condition |
No new damage, permanent deformation, or compromised seal after testing |
No damage or permanent deformation observed |
Pass |
| 18 |
Overall result |
Leak-test disposition |
All defined pressure, hold-time, pressure-decay, and visual criteria are met |
Bag accepted for the next processing step |
PASS |
Safety and validation note: The test pressure, hold time, pressure-decay limit, and connection method must be established and approved for the specific bag construction and application. Do not exceed the validated pressure rating of the bag or its components.
Check for Pressure Loss and Identify Possible Leaks
How to Perform a Leak Test on a 3D Transfer Bag?
A 3D transfer bag should be tested in a clean, controlled area. Confirm that the bag, tubing, ports, and seals are dry and undamaged. Close every connection firmly, then apply the pressure specified in the approved procedure. Never exceed the bag’s rated limit. Excessive pressure can create damage instead of revealing it. Record the starting pressure, time, temperature, and bag condition. A visible gauge makes small pressure changes easier to track.
Watch the gauge during the required holding period. Even a slight pressure drop deserves attention. Check the room temperature first, because cooling air can reduce pressure without causing a leak. Inspect folds, welded seams, tubing joints, and port caps. These areas often hide tiny channels. Gently reposition the bag so trapped folds become visible. Do not stretch it aggressively. That can produce a false result.
If pressure continues to fall, isolate each connection and repeat the test. A validated external leak-detection method may help locate escaping air. Avoid unapproved liquids on sterile components. A faint hiss, a growing bubble, or a damp patch can identify the leak point. Mark the location and remove the bag from service. Do not repair it unless the procedure specifically allows repair and requalification. The test is not perfect; gauge drift, poor closure, or uneven bag positioning can mislead the operator. Review the setup before rejecting good equipment or accepting a questionable result.
Document the Results and Safely Release Test Pressure
A leak test on a 3D transfer bag is useful only when its record is clear. Before testing, confirm the bag ID, lot number, operator, date, and test method. Record the starting pressure, ambient temperature, and planned hold time. Use a calibrated pressure gauge within its verified range. A handwritten value can become unclear later. Use a controlled form or validated electronic record. Include the connection points, tubing layout, and visible defects found before pressurization. Small details matter.
During the hold, record the actual start and end readings, not only “pass.” Note the pressure change, hold duration, and inspection result. Describe the bag’s shape, seams, ports, and protective overwrap. If pressure falls, stop and investigate. Do not quietly repeat the test until it passes. That weakens the record. A photograph of a questionable seam may support an investigation, but it cannot replace written observations. A second trained person should review the entries. This check often catches missing units or transposed numbers.
After approval, release pressure slowly through the designated vent or controlled outlet. Keep the bag secured and watch for sudden movement, fluid spray, or connector separation. Never open a clamp abruptly or press the inflated film by hand. Verify zero pressure on the gauge before disconnecting test equipment. Mark the bag’s status and retain the completed record according to site procedures. I have found rushed pressure release creates more uncertainty than the test itself. One imperfect note deserves correction, not concealment.
How to Perform a Leak Test on a 3D Transfer Bag?
Documented pressure-decay test record for a 3D transfer bag. The bag was stabilized at 300 mbar, monitored for 10 minutes, and evaluated against a maximum allowable pressure loss of 1.0 mbar during the test period.
Test result: Initial pressure was 300.0 mbar and final pressure was 299.4 mbar, giving a pressure loss of 0.6 mbar over 10 minutes. The recorded loss remained below the 1.0 mbar acceptance limit. After the final reading, test pressure was released slowly through the designated vent path before disconnecting any fittings.
FAQS
Examine the film, seams, ports, clamps, tubing, and protective caps under bright, angled light. Look for pinholes, scratches, creases, cloudy areas, and loose connections. Do not test visibly damaged bags.
Use a calibrated pressure gauge, regulated test gas, compatible tubing, and a timer. Confirm current calibration records. Prepare a clean, flat workspace without sharp edges.
Follow the validated procedure for that specific bag design. Never copy settings from another size. Pressure and duration must match approved test conditions.
Fully seat each fitting and secure every clamp. Close unused ports with verified caps or clamps. Support the ports gently. A loose fitting can imitate a bag leak.
Increase pressure gradually. Let the bag expand into a smooth, supported shape. Never open the regulator fully or stretch the film against nearby objects.
Watch the gauge, seals, ports, corners, and tubing junctions. Allow a short stabilization period before judging pressure changes. Continuous bubbles may indicate a leak when compatible detection solution is approved.
Record bag identification, batch details, equipment identification, operator, date, starting pressure, final pressure, temperature, and test duration. Keep the record clear. Missing details weaken the result.
Stop the test and inspect every connection, clamp, cap, and fixture. The fixture may be leaking. Repeat only through the approved investigation process, and document the outcome.
No. A stable gauge supports integrity, but it does not replace visual inspection. Small defects can remain hidden. I still recheck the fittings; it is easy to miss one.
Conclusion
How to perform a leak test on a 3D transfer bag? Begin by preparing the bag and the leak-test equipment in a clean, controlled work area. Carefully inspect the bag film, ports, tubing, connectors, and seals for visible damage, loose fittings, wrinkles, or contamination. Confirm that all connections are secure and that the test setup is appropriate for the bag’s specified pressure range.
Connect the bag to the test system and apply pressure gradually and evenly, avoiding sudden pressure changes that could affect the results or damage the assembly. Monitor the pressure for the required test period and check for any measurable loss. If pressure decreases, examine the ports, tubing, seals, and bag surface to help locate the possible leak. After testing, record the equipment settings, duration, observations, and final result. Finally, release the pressure slowly and safely before disconnecting the system and handling the tested bag.
 U-Care Medical