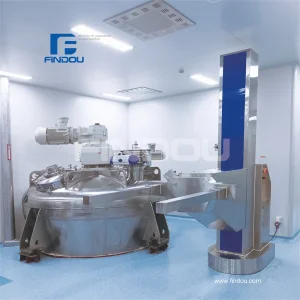
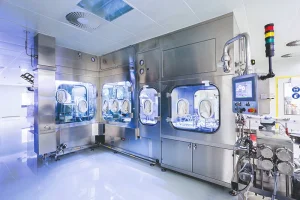
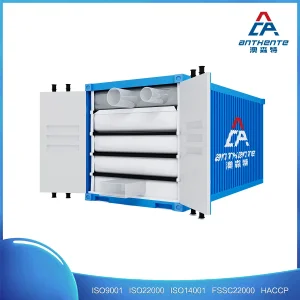
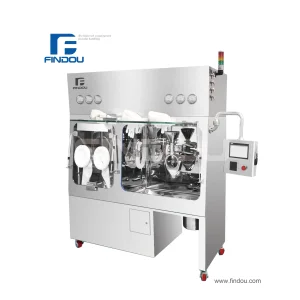
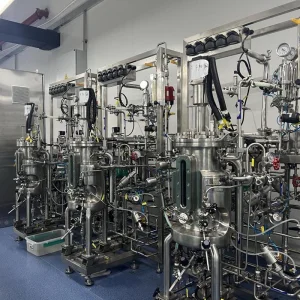
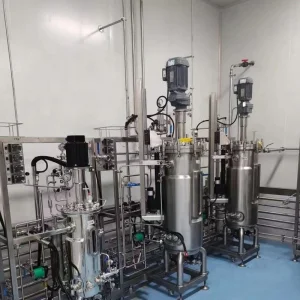
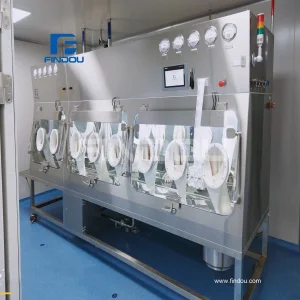
Explore our core product lineup engineered for absolute purity, airtight security, and compliance with stringent international standards.
Rooted in the Yangtze River Delta, delivering global standards in medical and pharmaceutical packaging solutions.
Changzhou U-Care Medical Co., Ltd. was established in 2014 and is located in Changzhou, Jiangsu Province, within the core region of the Yangtze River Delta—one of China’s most dynamic and economically advanced areas. Benefiting from a strategic location and convenient transportation network, the company enjoys strong access to both domestic and international markets.
U-Care Medical has accumulated extensive experience in the manufacturing of medical and pharmaceutical packaging products. The company is dedicated to the research, development, and production of high-quality disposable medical and pharmaceutical packaging materials. With a focus on innovation and reliability, U-Care strives to provide safe, efficient, and customized solutions to meet the evolving needs of healthcare and pharmaceutical industries worldwide.
The company is equipped with modern production facilities and adheres strictly to industry standards and quality management systems. From raw material selection to final product delivery, every step is carefully controlled to ensure product consistency, safety, and compliance with international regulations.
Guiding principles that drive our commitment to excellence in seamless storage solutions and medical packaging.
We always place product quality at the highest priority. Customer satisfaction is the driving force behind our continuous improvement and development.
We are committed to building long-term partnerships with our clients by adhering to honest and transparent business practices, never compromising on ethics or authenticity.
Through continuous innovation and refinement, we strive to develop more practical, reliable, and high-performance packaging solutions that support the stable and safe use of our customers’ products.
To become a trusted global provider of medical and pharmaceutical packaging solutions by consistently delivering superior quality, innovation, and customer-focused services.
To support the healthcare industry with safe, reliable, and efficient packaging products, contributing to better protection and delivery of medical products worldwide.
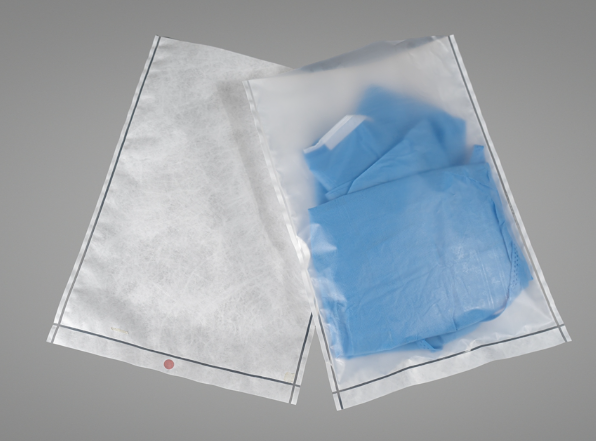
An authoritative analysis of structural engineering, supply chain resilience, and technological advancements in modern containment systems.
The global demand for high-integrity containment and distribution infrastructure has witnessed exponential growth. In sectors such as biopharmaceuticals, sterile API processing, advanced chemical manufacturing, and high-barrier food packaging, traditional welded or segmented storage units often introduce micro-crevices, potential points of contamination, and structural vulnerabilities. Seamless storage solutions engineered in China have emerged as the benchmark for absolute containment integrity.
By leveraging advanced multi-layer co-extrusion technologies, precision stainless steel fabrication, and computer-controlled cleanroom manufacturing environments, leading Chinese manufacturers deliver systems that ensure zero particulate shedding, superior gas-barrier performance, and optimized fluid dynamics. These developments directly address the rigorous standards mandated by FDA, EMA, and ISO regulatory bodies.
Global procurement directors increasingly source from Chinese manufacturers due to integrated supply chain ecosystems, rapid prototyping capabilities, and strict adherence to validation protocols (FAT/SAT). Partnering with certified innovators like Changzhou U-Care Medical ensures end-to-end traceability, custom engineering flexibility, and long-term economic scalability without compromising on clinical or industrial safety.
Discover our comprehensive range of high-performance connectors, isolator accessories, and specialized industrial equipment.
Expert answers regarding our manufacturing standards, custom solutions, and global export compliance.
 U-Care Medical