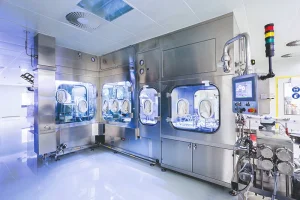
Explore our high-performance component engineering and sterile isolation systems designed for stringent pharmaceutical, fluid control, and industrial containment environments.
Backed by rigorous data parameters, manufacturing excellence, and global regulatory adherence to ensure enterprise-grade safety.
Comprehensive analytical insights into global regulatory changes, advanced polymers, and sustainable packaging infrastructure.
Rooted in innovation, driven by quality, and dedicated to global health protection.
We always place product quality at the highest priority. Customer satisfaction is the driving force behind our continuous improvement and development.
We are committed to building long-term partnerships with our clients by adhering to honest and transparent business practices, never compromising on ethics or authenticity.
Through continuous innovation and refinement, we strive to develop more practical, reliable, and high-performance packaging solutions that support the stable and safe use of our customers’ products.
To become a trusted global provider of medical and pharmaceutical packaging solutions by consistently delivering superior quality, innovation, and customer-focused services.
To support the healthcare industry with safe, reliable, and efficient packaging products, contributing to better protection and delivery of medical products worldwide.
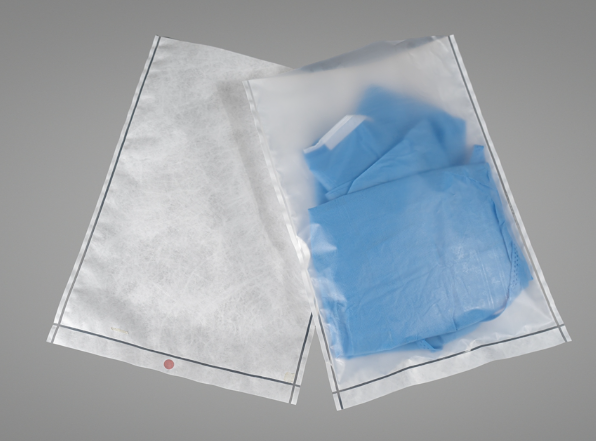
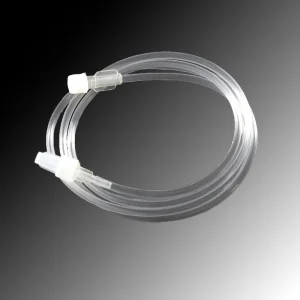
Discover our advanced sealing liners, geomembranes, high-vacuum fittings, and specialized industrial tubing systems.
Expert answers regarding our custom OEM non-toxic packaging solutions, manufacturing capabilities, and compliance standards.
We utilize certified medical-grade polymers, food-contact approved raw materials, and advanced extrusion techniques that completely exclude harmful plasticizers (such as phthalates), heavy metals, and toxic adhesives, ensuring full compliance with international safety regulations like USP Class VI and FDA standards.
Yes. With our advanced manufacturing infrastructure and dedicated R&D team, we offer comprehensive OEM and ODM services tailored to exact client specifications, including custom dimensions, specialized barrier coatings, unique sealing liners, and branded packaging structures.
Our solutions are widely deployed across the global pharmaceutical manufacturing, medical device sterilization, aseptic processing, food safety containment, and specialized industrial fluid transport sectors.
Operating under strict ISO quality management systems, every stage from raw material inspection and cleanroom extrusion to final product testing is meticulously monitored to guarantee absolute safety, consistency, and regulatory compliance.
 U-Care Medical