Explore our flagship clear barrier films, medical-grade cleanroom packaging, single-use bioreactor assemblies, and industrial processing machinery manufactured to stringent international quality specifications.

In today's global supply chains, the demand for high-performance Clear Barrier Films has experienced exponential growth. Historically, packaging systems requiring stringent protection against moisture, oxygen, and volatile organic compounds relied heavily on aluminum foil laminates. However, aluminum foil introduces significant operational limitations: it lacks optical transparency, prevents metal detector scanning on automated packaging lines, cracks under flexure (pinholing), and poses major challenges for circular economy recycling.
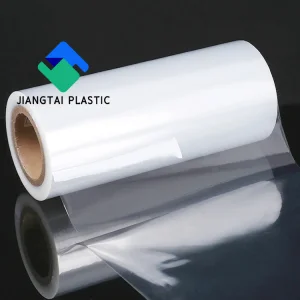
China’s leading barrier film manufacturers have pioneered advancements in nano-scale ceramic coatings (Silicon Oxide - SiOx, Aluminum Oxide - AlOx) alongside multi-layer co-extrusion technologies incorporating Polyvinylidene Chloride (PVDC), Ethylene Vinyl Alcohol (EVOH), Polyamide (PA), and Polyethylene (PE). These engineered clear barrier substrates achieve optical clarity exceeding 90% light transmission while suppressing Water Vapor Transmission Rates (WVTR) and Oxygen Transmission Rates (OTR) to pharmaceutical-grade thresholds.
Ultra-thin electron-beam evaporation deposits an invisible inorganic ceramic barrier (20–50 nm) onto PET or BOPP substrates. Provides stable barrier efficacy independent of relative humidity (RH) and is fully microwaveable.
Combines resins such as EVOH, PA, PP, and PE in a single step continuous blown or cast film process. Eliminates adhesive solvent residues, making it ideal for direct food contact and primary pharmaceutical packaging.
Engineered deep-draw thermoforming films designed for medical tray lamination and fresh food vacuum skin packaging (VSP). Delivers excellent mechanical puncture resistance and zero delamination under mechanical stress.
Selection of the optimal clear barrier structure depends on shelf-life duration, sterilization requirements (Autoclave, Gamma, EtO), mechanical flexibility, and end-of-life recyclability goals.
| Film Substrate Structure | WVTR (g/m²/24h @38°C, 90% RH) | OTR (cc/m²/24h @23°C, 0% RH) | Thermal Resistance | Key Application Focus |
|---|---|---|---|---|
| PET / SiOx Coating | 0.1 – 0.5 | 0.1 – 0.5 | Up to 180°C (High Retort) | Biopharma single-use bags, ready-to-eat microwave meals |
| PET / AlOx Coating | 0.3 – 0.8 | 0.5 – 1.0 | Up to 160°C | High-clarity window pouches, electronic component sealing |
| PA/EVOH/PE Co-extruded (9-layer) | 1.0 – 2.5 | 0.2 – 0.8 | Up to 121°C (Pasteurization) | Medical disposable packaging, meat & cheese thermoforming |
| PVDC Coated PET/BOPP | 0.8 – 1.5 | 1.0 – 3.0 | Up to 120°C | Pharmaceutical blister lidding, dry snack packaging |
| Mono-Material MDO-PE / EVOH-PE | 1.2 – 2.0 | 0.5 – 1.2 | Up to 100°C | 100% Recyclable high-barrier pouches (ESG Compliant) |
China has consolidated its position as the world's premiere manufacturing ecosystem for high-barrier films. Regional manufacturing clusters, particularly in the Yangtze River Delta region (Jiangsu, Zhejiang, Shanghai), provide global buyers with unparalleled vertical integration—from raw resin polymerization to precision multi-layer extrusion, vacuum coating, slitting, and cleanroom pouch fabrication.
Direct access to premium polymer supply chains reduces raw material procurement lead times and enables rapid compounding of custom barrier formulas tailored for specific gas permeability demands.
Top Chinese suppliers operate state-of-the-art machinery including W&H extrusion lines, BOBST vacuum metallizers, and Leybold SiOx coaters, maintaining precise micron-level thickness tolerances.
High production volume yields a total cost of ownership (TCO) advantage of 20% to 35% compared to North American or European converters without sacrificing optical purity or barrier stability.
When procuring clear barrier films for bio-pharmaceutical single-use assemblies or sterile medical device packaging, regulatory compliance is non-negotiable. Leading Chinese manufacturers operate under robust Quality Management Systems (QMS) aligned with international standards:
Comprehensive quality control tracking every roll of clear barrier film from raw resin lot numbers to finished roll quarantine and Certificate of Analysis (CoA) generation.
Full compliance with global direct food and pharmaceutical contact regulations. Rigorous overall migration testing (OMT) and specific migration limits (SML) verification.
Extrusion and pouch conversion conducted in positive-pressure cleanroom environments to eliminate bio-burden, particulate contamination, and pinhole risks.
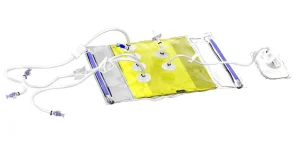
Biopharmaceutical production requires single-use bioreactor bags and 2D/3D liquid storage bags engineered with high-barrier films. These films must withstand cryogenic freezing (-80°C), gamma irradiation sterilization (up to 45 kGy), and mechanical stress during rocking agitation while maintaining near-zero leachables and extractables (E&L). EVOH and SiOx layered clear films provide total bio-compatibility for monoclonal antibody (mAb) and cell therapy processes.
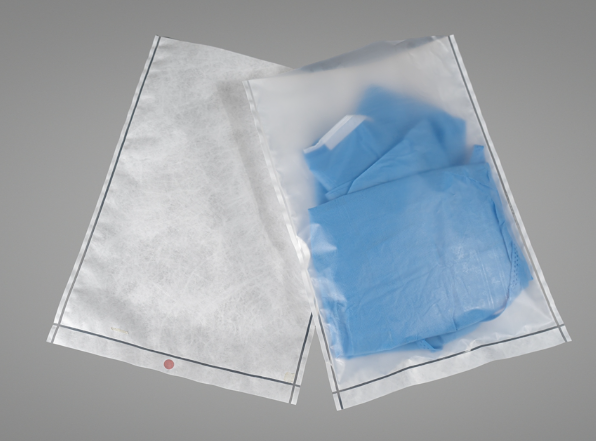
Catheters, infusion valves, orthopedic implants, and PCR diagnostic swabs demand peelable pouches and thermoformed blister packages with high puncture resistance and microbial barrier integrity. High-clarity PA/PE and Tyvek-laminated clear film configurations ensure immediate visual verification of product integrity before surgical deployment.
Transitioning from traditional tin cans and foil pouches to microwaveable clear barrier stand-up pouches allows consumers to view meal quality directly. SiOx and high-EVOH structures tolerate continuous thermal retort sterilization (121°C to 135°C) without barrier degradation or haze formation.
Changzhou U-Care Medical Co., Ltd. was established in 2014 and is located in Changzhou, Jiangsu Province, within the core region of the Yangtze River Delta—one of China’s most dynamic and economically advanced areas. Benefiting from a strategic location and convenient transportation network, the company enjoys strong access to both domestic and international markets.
U-Care Medical has accumulated extensive experience in the manufacturing of medical and pharmaceutical packaging products. The company is dedicated to the research, development, and production of high-quality disposable medical and pharmaceutical packaging materials. With a focus on innovation and reliability, U-Care strives to provide safe, efficient, and customized solutions to meet the evolving needs of healthcare and pharmaceutical industries worldwide.
The company is equipped with modern production facilities and adheres strictly to industry standards and quality management systems. From raw material selection to final product delivery, every step is carefully controlled to ensure product consistency, safety, and compliance with international regulations.
We always place product quality at the highest priority. Customer satisfaction is the driving force behind our continuous improvement and development.
We are committed to building long-term partnerships with our clients by adhering to honest and transparent business practices, never compromising on ethics or authenticity.
Through continuous innovation and refinement, we strive to develop more practical, reliable, and high-performance packaging solutions that support the stable and safe use of our customers’ products.
To become a trusted global provider of medical and pharmaceutical packaging solutions by consistently delivering superior quality, innovation, and customer-focused services.
To support the healthcare industry with safe, reliable, and efficient packaging products, contributing to better protection and delivery of medical products worldwide.
As international regulatory frameworks like the EU Packaging and Packaging Waste Regulation (PPWR) enforce circular economy compliance, traditional multi-material laminates (such as PET/ALU/PE) face increasing extended producer responsibility (EPR) fees.
China’s advanced clear barrier film manufacturers are leading the development of Mono-Material Polyolefin Structures (MDO-PE/PE or BOPP/PP) enhanced with nano-coatings or ultra-thin EVOH layers (< 5% total weight). These innovative films meet strict RIC 4 (LDPE) and RIC 5 (PP) recycling stream criteria while delivering oxygen and moisture barrier protection comparable to conventional multi-layer materials.
Key technical and commercial inquiries regarding procurement, compliance, and custom barrier film manufacturing.
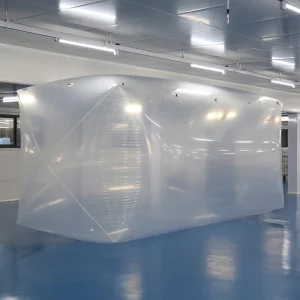
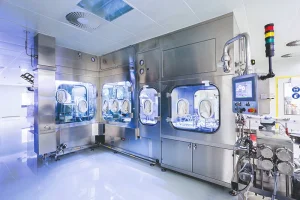
Browse our extended lineup of medical sampling tools, fluid transfer tubing, flexible isolators, and industrial packaging supplies.
 U-Care Medical